RFID tunnel and gate
Batch-reads the RFID tags inside a carton in one pass and checks the resulting tag list against the order; common in apparel and retail shipping and receiving.
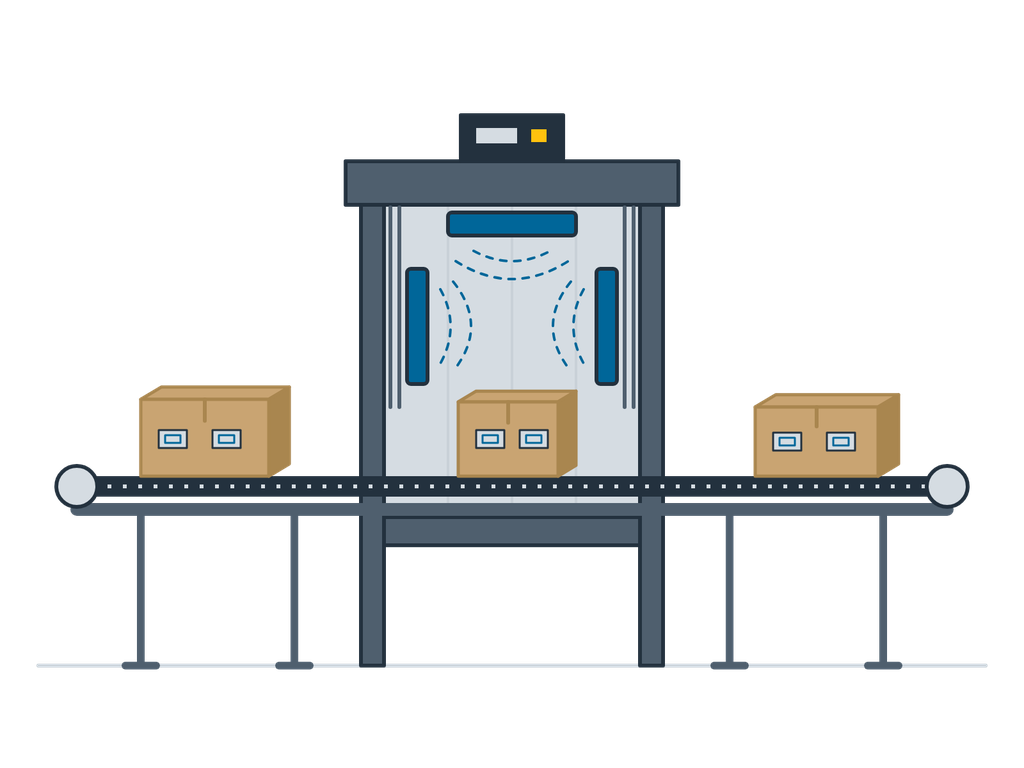
Batch-reads the RFID tags inside a carton in one pass and checks the resulting tag list against the order; common in apparel and retail shipping and receiving.
Batch-reads the RFID tags inside a carton in one pass and checks the resulting tag list against the order; common in apparel and retail shipping and receiving.
RFID reading comes in two forms: a shielded carton tunnel on a conveyor, and an open portal; the tunnel makes cross-reads easier to control. Both use several UHF antennas. As a carton passes, the RFID tags on the items inside are batch-read, without opening the carton or scanning item by item. Through EPC middleware, the list read is compared with the order or packing list, and surplus, missing or wrong items raise an alarm. It suits apparel and retail supply chains where every item already carries an RFID tag; the key is to stop reads from neighbouring cartons.
| Frequency | UHF |
|---|---|
| Type | Shielded tunnel on a conveyor, or a portal gate |
| Read rate | About 99.9% in vendor tests: 200 items per carton at up to about 1.2 m/s with about 0.9 m gaps, or 50–100 tags per carton at up to 50 m/min; must be verified on site |
| Conveyor speed | Vendor limits commonly about 40–50 m/min |
| Throughput | Vendor figures about 360–600 cartons/h, others up to 400; a case of about 1,000 cartons/h |
| Antennas | Several, set by carton type and read requirement |
| Output | Tag list per carton, checked against the order or packing list; alarm or reject on mismatch |
| Cross-read control | Shielded housing, automatic curtains and a minimum carton gap; speed, gap and reader power are tuned together |
Figures are typical configuration ranges; exact specifications are set per project.